Related Topics:
Solar Cell Packaging Adhesive-
Solar Cell Manufacturing Environmental Assessment Report
This white paper uses Life Cycle Assessment (LCA) to identify key environmental hotspots in the solar PV supply chain and offers strategies for reducing embodied carbon.
FAQs about Solar Cell Manufacturing Environmental Assessment Report
What impact do solar cells have on the environment?
It is identified that the majority of existing life cycle assessments on solar cells take into account four typical environmental impacts: energy consumption, greenhouse gas emissions, material depletion, and toxicity.
What is the manufacturing stage of solar cells?
4.6. Hotspots identification The manufacturing stage is identified as the hotspot during the whole life cycle of the solar cells. This stage is responsible for a large share of several environmental impacts, regardless of the type of solar cells.
What are the environmental impacts of a solar PV module?
A solar PV module using this technology has thin layers that contain materials such as CdTe and CdS. Here, Cd is the most toxic substance. It has substantial environmental impacts and its release into the atmosphere causes health impacts. Cd emissions from CdTe are around 0.26 g/GWh.
How to assess environmental impacts of PV systems?
Methods to assess environmental impacts The environmental impacts associated with PV systems can be estimated in two different ways. The first is by using conventional methods that deal with energy balance and carbon footprint calculation. The second is the use of advanced simulation tools that have the entire life cycle data inventory support.
Does solar PV supply chain impact environmental impact?
Nonetheless, assessment of environmental impact of production processes through the PV technology supply chain is essential to ensure its sustainability and this work outlines the environmental cost of solar PV supply chain for the US and China as leading global PV manufacturers with significant local reserves of silicon.
What are the environmental costs associated with silicon flows used in solar PV?
Data are available in Supplementary Information (#5). The environmental costs associated with silicon flows used in solar PV manufacturing include factors such as energy consumption, water usage, emissions of greenhouse gases and other pollutants, as well as the impact on local ecosystems and communities.
-
How heavy is a 500A solar cell
The wattages of solar panels can range greatly. While some solar panels power select appliances or RVs, others are powerhouses, and others can power industrial buildings. These solar panels differ in both size and. Here are some quick facts about the average weight of solar panels with differing wattages: 1. 100-watt solar panelsfrom 5 of the most. The roofs of current homes can safely support about 20 pounds per square foot. Including the mounting equipment, residential solar panels.
FAQs about How heavy is a 500A solar cell
How much does a 60 cell solar panel weigh?
Similar 60-cell polycrystalline panels typically weigh between 37 and 45 pounds (17 to 20 kilograms), which is a little less than monocrystalline panels. Thin-Film Solar Panels: Due to a different technology, thin-film solar panels are lighter than crystalline ones.
How much do solar panels weigh?
100-watt solar panels from 5 of the most popular brands average 18.8 pounds. 200-watt solar panels from 5 of the most popular brands average 23.28 pounds. Most 60-cell solar panels weigh about 44.9 pounds. Remember, these solar panels fall into the 270-300 watt range. 72-cell solar panels weigh around 61.73 pounds.
How much does A 72-cell solar panel weigh?
72-cell solar panels weigh around 61.73 pounds. As you may recall, these larger panels usually provide 350 to 400 watts. The weight of a solar panel per unit is an important consideration when deciding which size is best for your home, which we will discuss further in a later section.
How many solar cells are in a solar panel?
Multiple solar cells are assembled together to form a rectangular shaped panel. The standard solar panel size typically contains either 60 or 72 cells. You can also find panels with as few as 32 solar cells on recreational vehicles, as well as some larger commercial panels with as many as 96 cells.
How much does a residential solar system weigh?
Here is a summary of a residential solar system's typical weight: Solar Panels: The weight of solar panels for a residential system can vary from 40 to 60 pounds (18 to 27 kilograms) per panel, as was previously mentioned. Your energy requirements and the amount of space you have determine how many panels you need.
How much does a polycrystalline solar panel weigh?
They weigh around 30-40 pounds (13-18 kilograms). Polycrystalline panels are cheaper than monocrystalline panels, but they are not as energy efficient. They usually weigh around 42 pounds (20 kilograms). The cheapest option are amorphous (thin-film) panels.
-
12v solar cell fuse
For this reason, it's important to use fuses that are rated for at least twice the nominal voltage of your system; most 12V solar systems use fuses rated for 32 volts or more.
FAQs about 12v solar cell fuse
How do I choose a fuse for my DC Solar System?
Choosing a fuse for your DC solar system is not that difficult. Minimum fuse size is based on the load. Maximum fuse size is based on the current capacity of the wire. You then need to select a fuse in between these two.
What fuses do solar panels use?
Solar panels are almost always connected in what's called “series,” meaning that each panel adds its voltage to the others in order to produce higher total voltages . For this reason, it's important to use fuses that are rated for at least twice the nominal voltage of your system; most 12V solar systems use fuses rated for 32 volts or more.
How do you Fuse a solar panel system?
Properly fusing a solar panel system is a step-by-step process. Start by finding the fuse or junction box, usually near the inverter. Choose the right fuse type and amperage based on your solar panel specs. Remove the old fuse, noting its orientation. Check the wiring around for wear or corrosion before you go further.
What fuses do I need for a 12V 55W solar charger?
For a 12V 55W solar charger, you would need approx. 10A fuse. But please remember, my guess is based on the fact you give me and better safe than sorry. But if you find a 10A breaks too often, you can safely insert 15 or 20 A for cars also. Jst ensure you use appropriate wire gauge. 10A car fuses are fine for that.
What are solar panel fuses & breakers?
Solar panel fuses and breakers are critical components in any PV system. They provide protection against overcurrent and reverse current, ensuring that your system is safe from electrical hazards. Fuses are typically used in DC systems, while breakers are more common in AC systems.
How do I choose the right fuse size for my solar panel?
Choosing the right fuse size is vital, based on the system's worst-case current. For instance, a 144-watt 12V solar panel has a short-circuit current of 8.5 amps. To find the fuse size, add 25% for potential changes, making it 10.625 amps.
-
Solar Cell Manufacturing Industry Certificate
The International Electrotechnical Commission (IEC)certifications are widely recognized quality standard certifications throughout the solar industry. Following an overview about the major IEC PV module certifications: The IEC61215 covers the parameters which are responsible for the ageingof PV modules. This includes all forces of nature: 1. Sunlight incl. UV. 2. Climate (changing of climate, coldness, warmth, humidity). 3. Mechanical load (hail,. The IEC 61646 certification is for Thin-Film PV modules and is in many aspects identical to the international standard IEC 61215 for crystalline modules. An additional test takes the degradation behavior ofamorphous. IEC 60364-4-41 is about protection against electric shock for low-voltage electrical installations; it describes personnel safety measures for electrical systems. For photovoltaic systems it suggests total insulation,. Photovoltaic (PV) module safety qualification, which was later issued as the European standard EN 61730 (almost similar). The IEC / EN 61730 consists of 2 parts: the first part covers.
[PDF Version]
FAQs about Solar Cell Manufacturing Industry Certificate
What are the common ISO certificates for the solar industry?
The common ISO certificates for the Solar industry include- ISO 9001 helps in the implementation of Quality Management System in an organization so that the product meets the customer's expectations in terms of quality. It brings about confidence among the stakeholder regarding the quality of the products as well as processes.
Do solar PV installations need to be MCs certified?
Also, the Council of Mortgage Lenders has advised that, as a minimum to avoid the risk of a property being ineligible for a mortgage, both new and existing Solar PV installations must be MCS certified. All renewable energy products are examined by certification bodies against MCS manufacturing and testing standards.
What are the major IEC PV module certifications?
Following an overview about the major IEC PV module certifications: The IEC61215 covers the parameters which are responsible for the ageing of PV modules. This includes all forces of nature: Climate (changing of climate, coldness, warmth, humidity).
What is Microgeneration Certification Scheme (MCS)?
Microgeneration Certification Scheme (MCS) is the main accreditation body for small-scale, low-carbon, and renewable technologies in the UK such as solar PV, biomass, wind turbines, and heat pumps. MCS certifies, quality assures, and provides consumer protection for microgeneration installations and installers.
How many GW of solar modules are there?
With over 3GW of modules shipped globally in the past 33 years, our modules power some of the biggest industry and utility scale projects in North America and Europe in addition to India. Worried about ever-increasing energy costs?
What is the production capacity of our module manufacturing lines?
Our module manufacturing lines have an in-house production capacity of 670MW for modules and 530MW of cells, can process both mono of 182mm and multi-crystalline cells of 158.25mm sizes.
-
4ah solar battery cabinet lithium battery pack single cell capacity
Ample Storage Capacity: The 4-slot design allows you to store up to four lithium iron phosphate batteries in a single cabinet. This helps optimize space utilization and minimizes clutter, providing a neat and organized storage solution. More than 90% of the time, the output voltage is about from 24V to 26V in one of discharge cycle. At CooliBattery, we specialize in manufacturing and supplying high-performance LiFePO4 home energy storage systems designed for solar applications, off-grid living, and residential backup. Our core products include wall-mounted batteries, rack-mounted lithium storage, and Energy Storage Cabinet. Redarc's smart charging system delivers reliable battery power through every leg of the journey - whether you're. LiFePO4 1-4S. PAC Battery provides one-stop service and various batteries, such as: • Home storage battery: Wall mounted type, wheel stand type and stackable type; 24V 5kWh, 24V 10kWh, 48V 5kWh, 48V 7kWh, 48V 10kWh, 48V 20kWh, 400V 8kWh, 400V 12kWh, etc • Commercial solar battery: rack type battery in cabinet;.
[PDF Version]
-
What major should I study for solar photovoltaic panel packaging
Solar panels are typically either horizontally or vertically stacked in a box. Usually, separatorsare placed between each module, and extra protections are added to the four corners of each module stack. In some cases, modules are also packed in individual cartons boxes to be packed into a large master carton box. Horizontally stacked each on top of each other can cause stresses on the panels below that can lead to defects clients do not detect for a long time,. With loading, transport and unloading there lie more dangers ahead:improperly packed, the mechanical stresses and risks the panels are exposed to during their long journey are multiple,.
FAQs about What major should I study for solar photovoltaic panel packaging
What will I learn in a photovoltaic (solar panel) course?
In a photovoltaic (solar panel) course, you will learn to identify the key components needed in a basic solar panel system, such as those found on a house or building and explain the function of each component in the system.
Are there any companies specializing in solar (PV) module packaging?
There already exist some companies specializing in solar (PV) module packaging, offering advanced packaging materials and sound packaging solutions. There will be global standards at a certain point in time to which more and more manufacturers will adhere.
Do solar panels need packaging?
There are PV manufacturers that reduce their costs to a minimum when it comes to the packaging. There are known cases of pallets of solar panels that were simply covered in plastic. There are better and safer ways to transport your panels. For more details read our feature article on solar panel packaging.
How are solar panels packaged?
This brief article is an introduction to solar panel packaging. Solar panels are typically either horizontally or vertically stacked in a box. Usually, separators are placed between each module, and extra protections are added to the four corners of each module stack.
What is the best packing material for solar panels?
Common solar panel packing material is corrugated cardboard boxes. Cardboard boxes are common with 2 panels in one box, or large cardboard boxes, as displayed on the image below.
Do solar panels need to be packed safely?
Correct and safe solar panel packing is an important, yet mostly neglected aspect of the post-solar panel production process. After the solar panels have been produced, being an overwhelmingly export-heavy product, they need to be packed safely, as the transport on the road, sea and air can be rough.
-
What is the difference between solar cell grade A and grade B
Grade B solar panels have some visual defects that do not affect performance. Grade B naturally falls below grade A in this grading system. So how does Grade B stack up against the other grades? Grade A solar panels are entirely free of defects. Grade B has some visual flaws but still meets performance standards. Grade C. Like elementary school, solar panels are graded on several factors, mainly visual and performance flaws. While this grading system follows similar logic, different manufacturers and distributors can have other criteria for their grading systems. Before buying any solar. So, which type of solar panel suits your needs best? The performance and pleasant appearance of grade A solar panels? The ugly appearance, yet the excellent performance of the grade B solar panels? Or can you get a group of grade C solar panels entirely free?. At the heart of the grading system are defects. These defects in solar panels are the basis for how they are graded, and knowing them can help you determine your grading stem for.
[PDF Version]
FAQs about What is the difference between solar cell grade A and grade B
What is the difference between Grade A and grade B solar cells?
Such modules usually have only a positive tolerance (i.e. the capacity of the modules is always higher than the passport one) and lower temperature coefficients. Grade B solar cells have visual defects and have a lower filling factor of the CVC characteristic: 0.4-0.7. Their price is usually a bit lower than that of the elements of Grade A.
What is a Grade B solar panel?
Grade B solar panels have visual defects but meet performance specifications. These solar panels are less common than grade A solar panels but are typically available from manufacturers upon request. Most manufacturers keep these panels for testing purposes but sell them with warranties like grade A solar panels.
What does grade a mean on a solar panel?
Grade – A normally means a panel has no visible defects and all the major possible defects are covered by manufacturer's standard warrantyl. Grade – B usually means the panel has some “cosmetic imperfections” or “cosmetic blemishes” of the above, but has the “same” electrical output as Grade – A.
Do grade B solar panels affect performance?
Grade B solar panels have some visual defects that do not affect performance. Grade B naturally falls below grade A in this grading system. So how does Grade B stack up against the other grades? Grade A solar panels are entirely free of defects. Grade B has some visual flaws but still meets performance standards.
Are Grade A solar panels a good choice?
Ultimately, it comes down to this: Grade A solar panels have no visual defects and meet performance standards. Grade B solar panels have some visible defects but meet performance standards. Grade C solar panels have visual defects and do not meet performance standards. Grade D solar panels are unusable, and entirely broken.
What are Grade C and grade D solar panels?
Grade C and Grade D panels occupy a niche in the solar panel spectrum, and their use is relatively rare: Grade C Panels: These panels often have severe cosmetic flaws or are made from cells with visible damage. They are typically unsuitable for standard solar installations.
-
Semi-soft film solar panels
Thin-film solar cells, often called amorphous solar panels, are much thinner and more flexible than traditional ones. They're made to easily blend with different surfaces.
FAQs about Semi-soft film solar panels
What are thin film solar panels?
Thin-Film Solar Panels: Thin-film solar panels are lightweight and highly flexible. They're made by depositing a thin layer of photovoltaic material onto a substrate. These panels are suitable for curved surfaces and temporary installations due to their flexibility.
What is a thin-film solar PV system?
This is the dominant technology currently used in most solar PV systems. Most thin-film solar cells are classified as second generation, made using thin layers of well-studied materials like amorphous silicon (a-Si), cadmium telluride (CdTe), copper indium gallium selenide (CIGS), or gallium arsenide (GaAs).
What materials are used for thin-film solar technology?
The most commonly used ones for thin-film solar technology are cadmium telluride (CdTe), copper indium gallium selenide (CIGS), amorphous silicon (a-Si), and gallium arsenide (GaAs). The efficiency, weight, and other aspects may vary between materials, but the generation process is the same.
What are the applications of thin-film solar technology?
One of the most important applications for thin-film solar technology, specifically Copper Indium Gallium Selenide (CIGS) and Gallium Arsenide (GaAs) technology is the space applications.
What is the difference between crystalline silicon and thin-film solar panels?
There are many differences regarding crystalline silicon and thin-film solar panel technology. One important difference is how the temperature affects the efficiency of each technology, c-Si solar cells are more affected by temperature than thin-film technologies.
How are CIGS thin-film solar panels made?
Manufacturing for Copper Indium Gallium Selenide (CIGS) thin-film solar panels has improved throughout history. Currently, CIGS thin-film solar cells are manufactured by placing a molybdenum (Mo) electrode layer over the substrate through a sputtering process. The substrate is usually manufactured with polyimide or a metal foil.
-
The first solar cell efficiency
Those first silicon solar cells were about 6 percent efficient at converting the energy in sunlight into electricity, a huge improvement over any previous solar cells.
FAQs about The first solar cell efficiency
What is solar cell efficiency?
Solar-cell efficiency is the portion of energy in the form of sunlight that can be converted via photovoltaics into electricity by the solar cell. The efficiency of the solar cells used in a photovoltaic system, in combination with latitude and climate, determines the annual energy output of the system.
When did solar cells become more efficient?
In 1985, researchers at University of New South Wales, Australia were able to construct a solar cell that has over 20% efficiency. A 20% efficiency solar cell were patented in 1992. In the 21st century, the efficiency continues to rise and and the future forecast shows that there are no signs that the efficiency would stop increasing.
When did photovoltaic cells become more efficient?
In 1955, Hoffman Electronics-Semiconductor Division introduced photovoltaic products with only a 2% efficiency, with an energy cost of $1,785/Watt (USD). In 1957, Hoffman Electronics were able to introduce cells with an increased efficiency, at 8%. The same company's solar cell efficiency was increased to 9% in 1958 and 10% in 1959.
When was the first solar cell made?
The first solar cell using silicon monocrystalline was constructed in 1941. Early silicon solar photovoltaic sells did not, however, have good efficiency.
What paved the way for further improvements in solar cell efficiency?
Breakthroughs such as the discovery of the photovoltaic effect and the development of the first silicon solar cell paved the way for further improvements in solar cell efficiency. Solar cell efficiency refers to the ability of a solar cell to convert sunlight into electricity.
Who invented photovoltaic solar cells?
At Bell Telephone Laboratories in Berkeley Heights, NJ, Daryl Chapin, with Bell Labs colleagues Calvin Fuller and Gerald Pearson, invented the first practical photovoltaic solar cell for converting sunlight into useful electrical power at a conversion efficiency of about six percent.
-
What are the solar cell energy storage cabinet for solar-powered communication cabinets
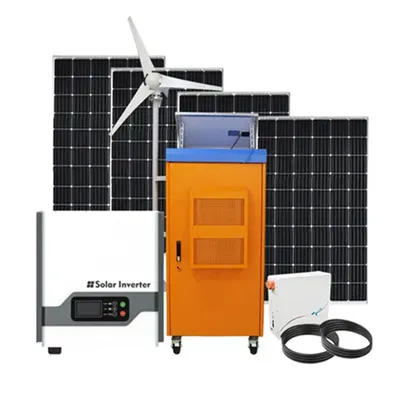
Multi-energy complementary systems combine communication power, photovoltaic generation, and energy storage within telecom cabinets. Remote diagnosis, performance tracking, and fault alerts through intelligent BMS. Versatile capacity models from 10kWh to 40kWh to. Highjoule's site energy storage solution delivers stable, efficient, and intelligent power for diverse application scenarios. You might be a telecom infrastructure manager, a green energy consultant, or perhaps someone tired.
-
Photo of solar cell fracture
An innovative image analysis technique is proposed to process real solar cell pictures, identify grains and grain boundaries in polycrystalline silicon, and finally generate finite element meshes. Using a modified intri. Photovoltaics (PVs) based on silicon semiconductors is the most growing technology i. 2.1. Image analysis of solar cellsThe majority of produced solar cells are made of either mono or polycrystalline silicon. The material microstructure has a role on the electri. For the numerical simulation of transgranular and intergranular cracking in polycrystalline silicon, a 2D plane stress model is considered. The principle of virtual work reads:(1)∫V(. A model problem consisting of 4 grains (lateral size of about 1 cm) is analyzed under plane stress conditions with a typical thickness of solar cells equal to 0.166 mm. Three different F. A computational framework for the simulation of intergranular and transgranular cracking in polycrystalline silicon solar cells has been proposed in the present work. To.
[PDF Version]
FAQs about Photo of solar cell fracture
Do cracks and fractural defects in solar cells cause hotspots?
This work investigates the impact of cracks and fractural defects in solar cells and their cause for output power losses and the development of hotspots. First, an electroluminescence (EL) imaging setup was utilized to test ten solar cells samples with differing crack sizes, varying from 1 to 58%.
How does a finger fracture affect a solar cell?
According to the research results, the finger fracture affected the series resistance of the solar cell and output power by simultaneously changing the spatial distance of the finger and the number of fingers.
Are solar cells affected by different crack sizes?
Furthermore, we have also considered studying different solar cells affected by different crack sizes (1–58%), which is different from other recent research work 26, 31, which only considered studying PV module-level cracks (i.e., they did not investigate solar cell-level cracks vs crack sizes).
What is a crack in a solar cell?
Often cracks are named microcracks or µcrack, and all typically indicate a fracture in the solar cells in the range of mm to as small as in micrometres. Both terms usually suggest the same type of cracks where partially fully isolated areas are developed in the solar cells mainly due to mechanical or thermal stresses 3, 4.
Do solar cell cracks cause power loss?
This effect is usually ignored when examining solar cell cracks 31, 32, 33. Another contribution of this work is that we have presented the results of the output power degradation of two solar cell samples under the PID test. We have then correlated the power losses of the PID test results with the cracked solar cell samples.
Does a photovoltaic module have a finger fracture?
The finger fracture model was applied to the entire photovoltaic module. According to the actual photovoltaic module finger fracture, we analyzed the case when the photovoltaic module had a finger fracture of 10% with an average power loss of −0.99%.